
- Cpk 1.851 (one characteristic on one part, not a blanket capability claim) on a representative length characteristic (76.1–76.5 mm), against an initial-study target of Ppk ≥ 1.67.
- 20+ inspection instruments, including two Hexagon CMMs, a KEYENCE laser microscope, and an XRF spectrometer.
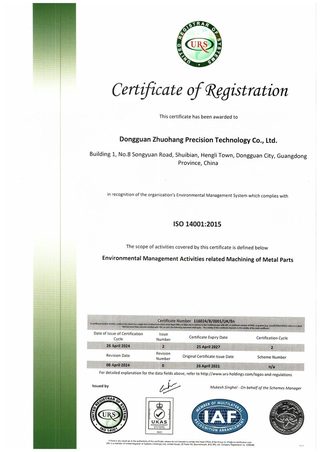
- Three certificates with numbers — ISO 9001, IATF 16949, ISO 14001 — issued by URS and verifiable.
- Full lot traceability from raw material to shipment, with XRF material verification at incoming.
Read the tolerance band before you read the index. Cpk is a ratio of the tolerance band to the process spread, not an absolute measure of accuracy. The figure above was recorded on a length characteristic with a 0.4 mm band (76.1–76.5 mm) — wide by design. Hold the same process spread against a ±0.005 mm feature and it fails outright. Ask for the band, the subgroup count and the sampling window on every capability number a supplier quotes.
Why is quality the biggest hidden bucket in total cost?
A reject discovered after shipping does not cost the price of the bad part — it costs the remake, the re-inspection, the expedited freight to catch the schedule, and possibly a stopped line while you sort the batch. A small reject rate, applied across a year of parts, can erase the entire savings of a cheap unit price. That is why, in the total-cost equation, process capability matters more than the number on the quote.
The rest of this page is the evidence that keeps that bucket near zero: process control, verified material, documented inspection, and traceability. Each one is a cost you do not pay.
What certifications back the quality system?
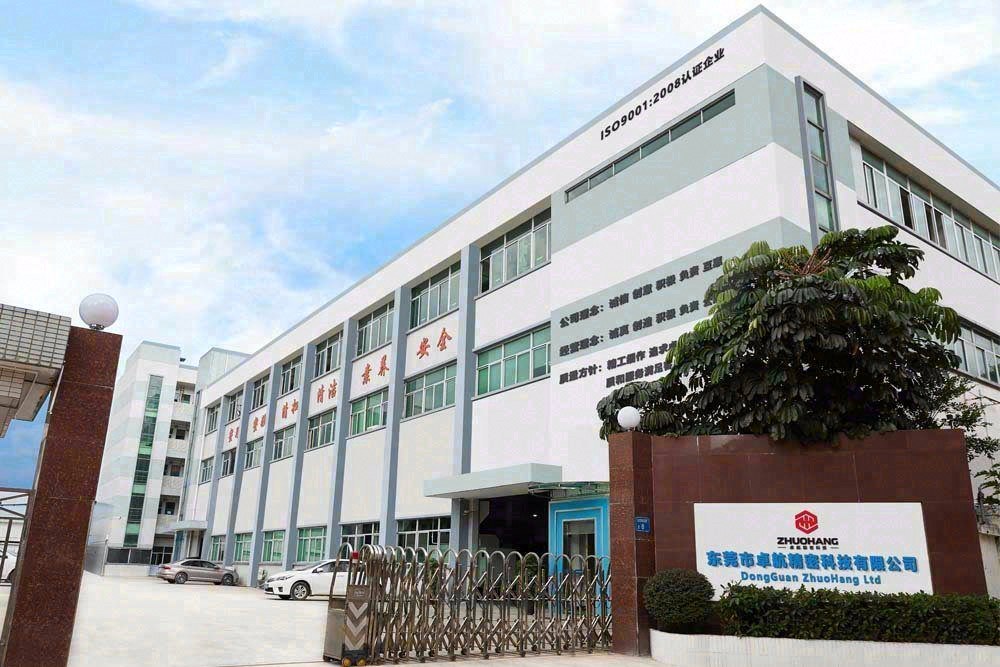
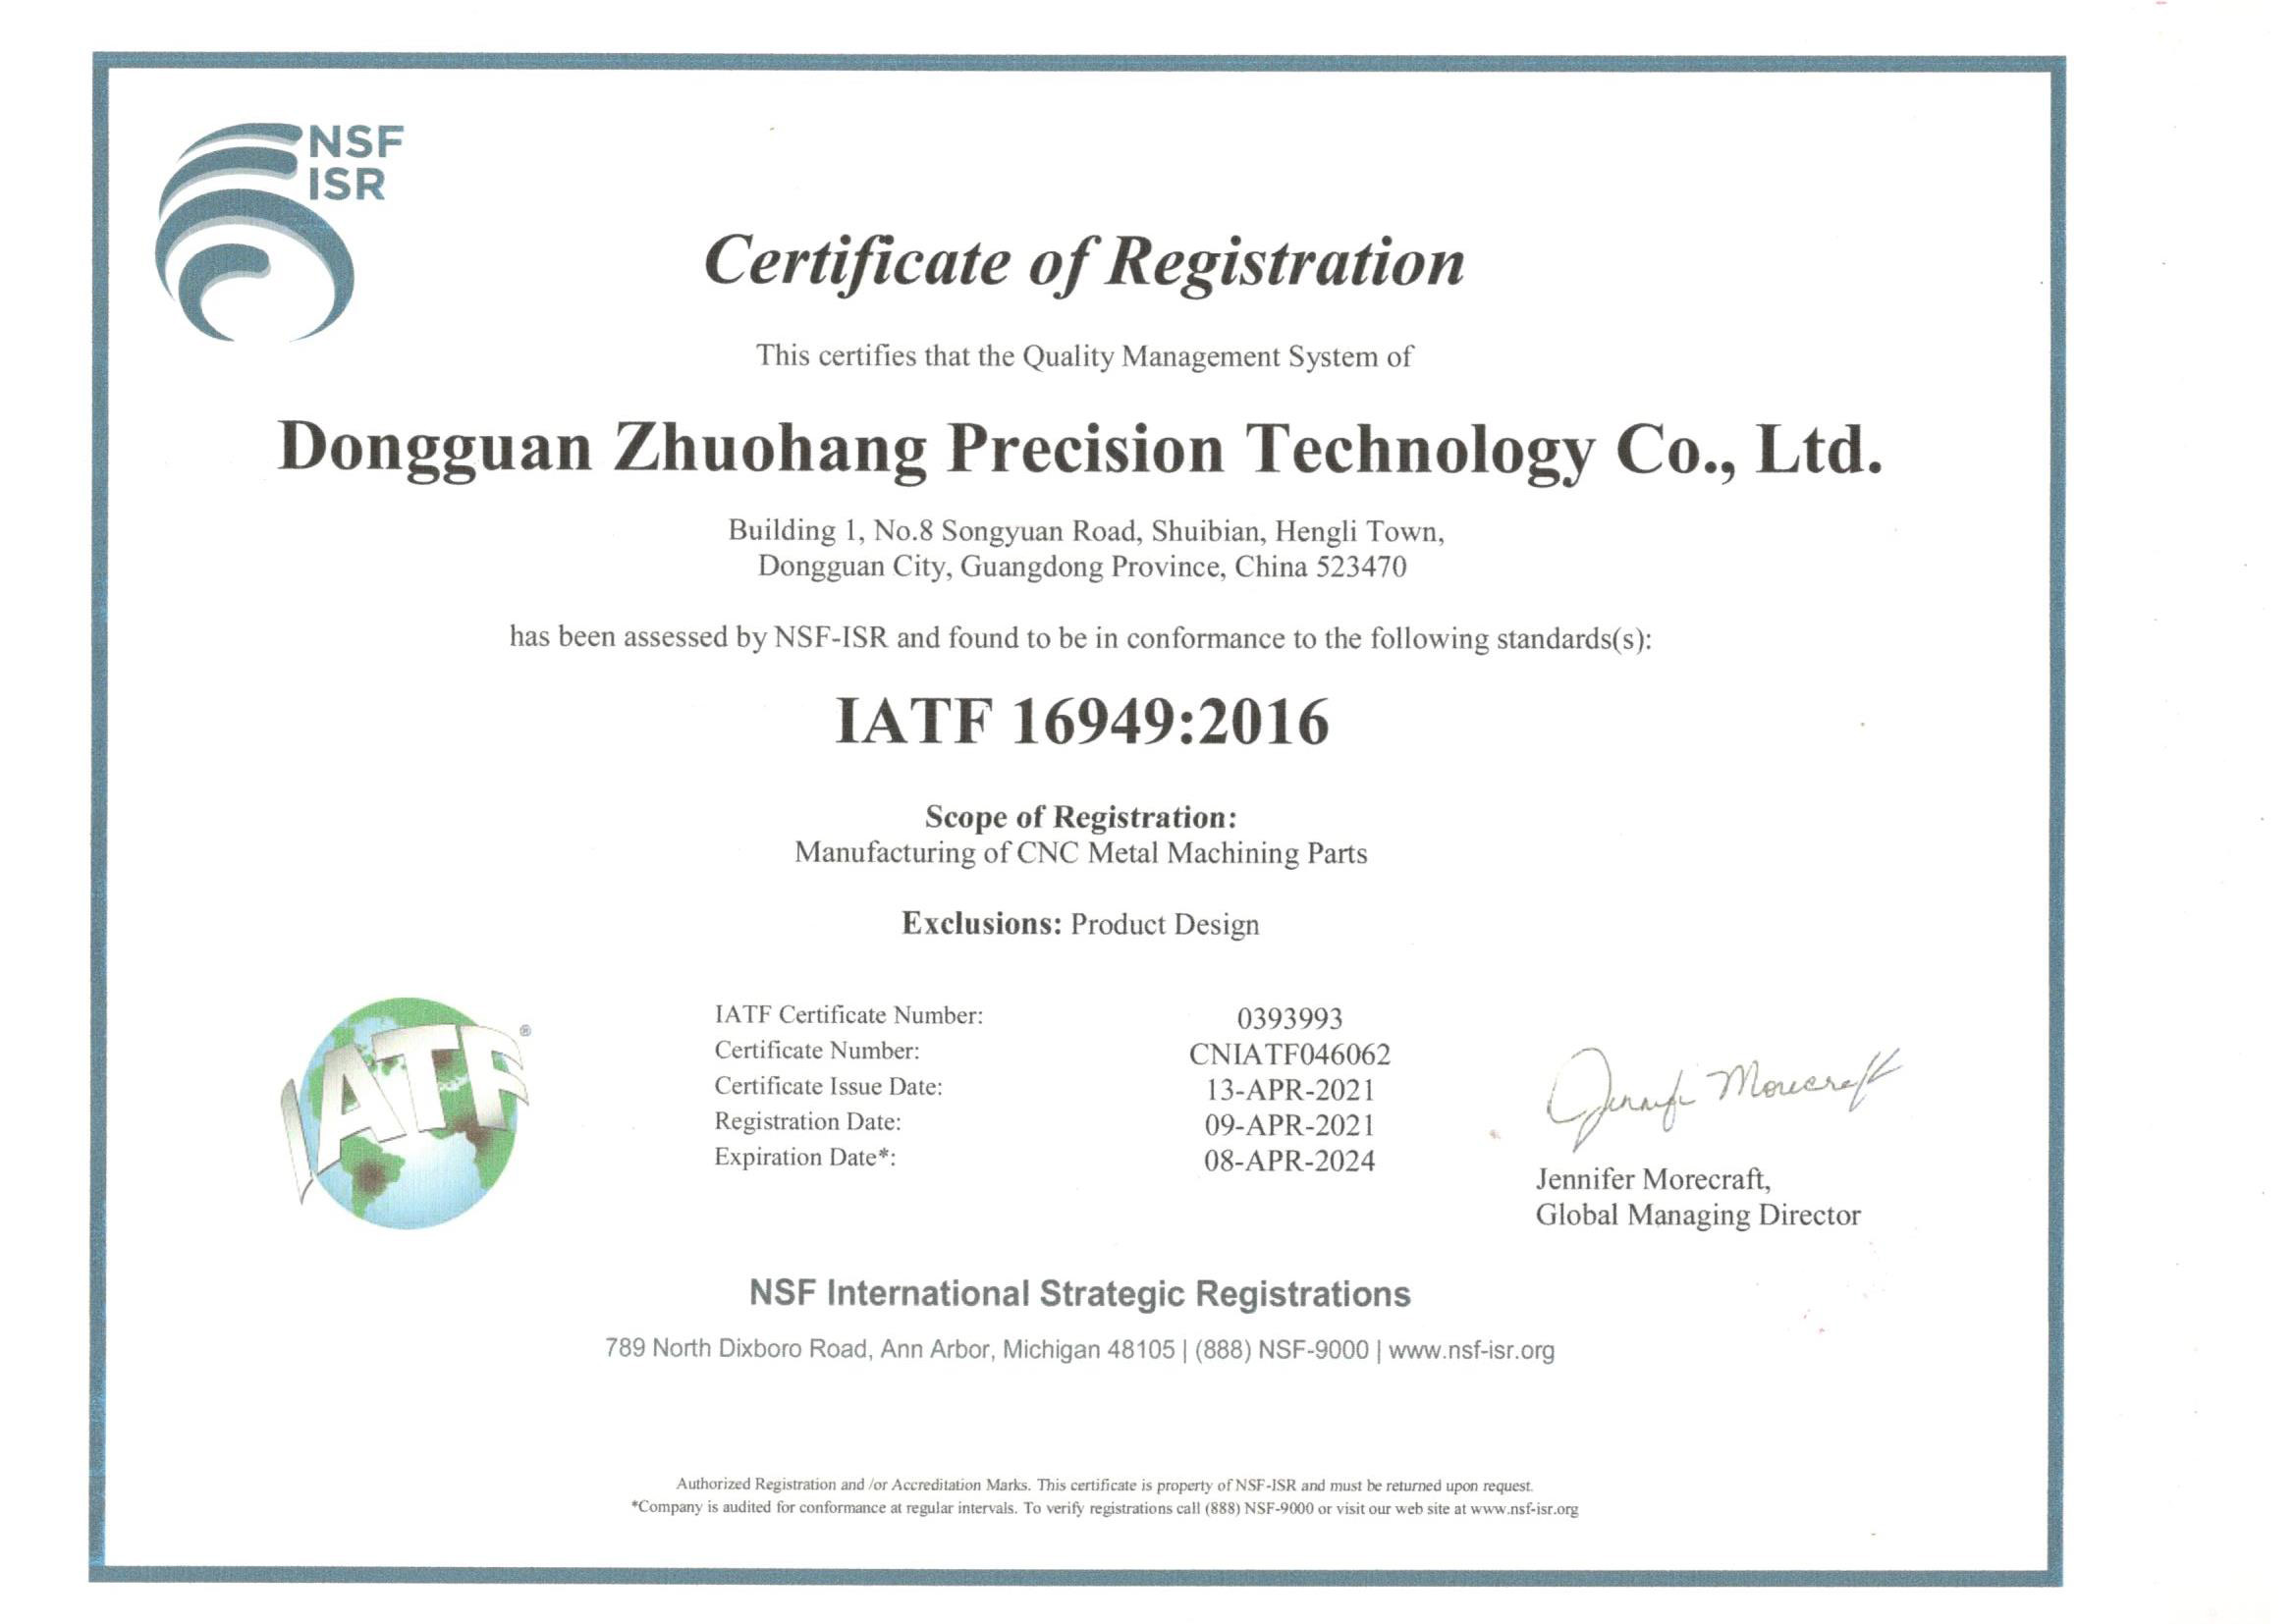
A certificate is only as good as the number you can check with the registrar. Three third-party-certified systems govern production here, each issued by URS and verifiable.
| Standard | Certificate number | Scope |
|---|---|---|
| ISO 9001:2015 | 116024/A/0001/UK/En | Machining of metal parts |
| IATF 16949:2016 | 131941/A/0001/SM/En | Manufacture of CNC metal machining parts (excludes product design, Clause 8.3) |
| ISO 14001:2015 | 116024/B/0001/UK/En | Environmental management related to machining of metal parts |
Why IATF 16949 matters to your cost model: it is the strictest quality-management standard in volume manufacturing, and the SPC, FMEA, and control-plan discipline it requires runs on every job here, not just automotive ones. That discipline is what keeps rejects near zero, which is the whole point of buying it.
How is process capability proven, not claimed?
A tolerance printed on a page proves nothing. A control chart proves the process is stable and predictable, that it will keep producing good parts, not that one sample passed. Here is the real SPC result this facility works to:
| Characteristic | Spec range | Subgroups | X̄ | Cpk | Judgement |
|---|---|---|---|---|---|
| Length | 76.1 – 76.5 mm | 25 × 4 | 76.393 | 1.851 (one characteristic on one part, not a blanket capability claim) | OK |
The internal standard is Ppk ≥ 1.67 initial on key characteristics and Cpk ≥ 1.33 on general ones. A Cpk of 1.851 (one characteristic on one part, not a blanket capability claim) sits comfortably inside spec. For you, that number is the cost of quality failure trending toward zero, and it is the figure you should ask any supplier to show before you compare prices.
Cpk maps to the distance between the process mean and the nearest tolerance limit, measured in standard deviations, which is why a higher Cpk means a process that can drift further before it produces a reject. The ladder below is how an auditor reads the number.
| Cpk | Meaning | Reject implication |
|---|---|---|
| 1.00 | Process mean sits at the tolerance edge | Rejects imminent with any drift |
| 1.33 | Minimum stable-production bar | Low rejects while the process stays centered |
| 1.67 | Key-characteristic target | Very low rejects, tolerant of drift |
| 2.00 | Six-sigma class | Rejects designed out of the process |
A supplier that quotes a Cpk is making a statistical claim you can audit against its raw subgroups. Ask for the mean and range behind the headline number — a real chart has a measured mean and a measured spread, while a made-up one has only the number. The audit takes minutes and separates a stable process from a lucky sample every time.
How do you prevent mixed-lot material scrap?
One of the cheapest ways to lose money on metal parts is to machine the wrong alloy and find out at inspection. The prevention is at the door: every incoming lot is XRF-checked against its mill certificate before it reaches a machine, so a mixed lot is caught before a single chip is cut. That one step removes an entire class of scrap that a buyer would otherwise pay for in rejects — a hidden bucket emptied at the source.
Which inspection instruments verify dimensions?
Verification is only as good as the instruments behind it, and the bench here is the same class a buyer would use to audit the shop:
- Hexagon GLOBAL S CMMs (2) — dimensional verification on 3D geometry.
- KEYENCE VK-X3000 laser microscope — surface profile and micro-feature measurement.
- SURFCOM 1800D — surface roughness and contour.
- iCHEQ XRF spectrometer — alloy composition against the mill certificate at incoming.
- Micro-Vickers hardness tester, Fischer coating-thickness gauge, salt-spray chamber, tensile tester — material and finishing verification.
- Gear measuring center and vision measuring machines — complex and micro geometry.
Named instruments matter for the same reason named machines do: they are inventory, not adjectives. A shop that can tell you it verifies parts on two Hexagon CMMs and checks alloy on an XRF spectrometer is a shop with a real bench; a shop that says "we inspect every part" is describing an intention. The nameplate is the audit trail — you can ask to see the instrument, read its calibration record, and watch a measurement run, which turns a quality claim into a verifiable fact.
Can parts be traced back to the raw material?

For regulated buyers, traceability is the difference between an isolated lot and a recall, and a recall is the worst line in any total-cost model. The MES/ERP system records the full chain on every job: raw material source and usage, process parameters, machine data, production batch, machining time, operator, and inspection results. If a non-conformance ever surfaces, the record names the exact lot, machine, and operator, so the impact is isolated instead of guessed.
What quality documents ship with the parts?

Documentation is the part of quality that reduces your supplier-management cost: instead of re-measuring every shipment, your team confirms the record. Depending on the program, the shipment includes a first-article inspection report, a CMM dimensional report, SPC control charts, and the material certificate. The result is that incoming inspection becomes a check of evidence rather than a second full measurement — a direct saving in a bucket most buyers never see.
How do tolerance and surface-finish standards anchor the quality record?
A quality record only means something when it is measured against a standard, not against a claim. The two standards a machined-part buyer sees most often are the ISO 2768 general tolerances and the Ra surface-roughness scale. Knowing where a print sits on each ladder tells a buyer whether the shop is over- or under-committing on precision, which is a quality cost signal in either direction.
| Call-out | Typical process | Relative effort |
|---|---|---|
| ISO 2768-m (general) | Standard machining | Baseline |
| ISO 2768-f (general) | Careful machining | Slightly higher |
| ±0.003 mm (milling) / ±0.002 mm (turning) | SPC-controlled CNC plus CMM | High — milling and turning |
| ±0.002 mm | Precision grinding | Highest — grinding |
Surface finish runs on the Ra scale and follows the same ladder. Ra 3.2 µm is a normal milled or turned result; Ra 1.6 µm takes a careful pass; Ra 0.8 µm and below needs grinding or polishing, which is exactly where a bearing seat or a sealing face earns its finish and a cosmetic surface does not. A shop that reads these two ladders correctly spends your quality budget where the part needs it, and that discipline is what keeps the quality-failure bucket near zero without over-charging the unit price.
What quality signals should make a buyer walk away?
The quality-failure bucket almost always announces itself before it bills you, if you know what to look for. A supplier that is about to hand you rejects will avoid producing the evidence of process control, will be vague about how it verifies material, and will describe its inspection in adjectives rather than instruments. The signals are consistent because the behaviors that create rejects are the same behaviors that hide them.
- A tolerance claim without a CMM or SPC record. Precision is a measurement, not an adjective. Ask for the chart from a real job.
- Material verification described as "we check it." The check that matters is an XRF read against the mill certificate, with a record you can pull up.
- An inspection bench with no names. A real bench names its CMM, its profilometer, its XRF; a vague one is a brochure.
- Traceability described in general terms. Ask for the record on a specific lot, and watch how fast it comes back.
Each signal is a chance to stop before the reject lands on your dock. The buyer who runs this list during the first exchange spends five minutes and avoids the most expensive bucket in the total-cost model; the buyer who skips it finds out the expensive way, after the invoice.
What this shop actually runs
Ask for capability evidence and the answer should be specific. The facility behind this guide runs 100+ CNC machines on a 6,800 m2 floor in Dongguan, China, with 100+ staff. The machine list, by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Matched to compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Matched to prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Matched to long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Matched to shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Matched to hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerances held: milling ±0.003 mm, turning ±0.002 mm, grinding and wire EDM ±0.002 mm. Capability: Ppk >= 1.67 initial and Cpk >= 1.33 in production on key characteristics.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, clause 8.3 design excluded, disclosed openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, USCC 91441900MA4UWT6X39, established 2005.
Service area: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — built in China, shipped worldwide.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Ask to see the quality evidence behind the price
Request a sample CMM report and SPC chart — email [email protected] or call +86 13126536955.
Frequently Asked Questions
Why is quality the biggest hidden bucket in total cost?
In short, Because a reject discovered after shipping costs the remake, the re-inspection, the expedited freight, and possibly a stopped line, not just the price of the bad part. A batch with a small reject rate can erase a year of cheap prices, which is why process capability matters more than unit price.
What certifications back the quality system?
In short, ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En), and ISO 14001:2015 (116024/B/0001/UK/En), all issued by URS. The IATF 16949 scope excludes product design under Clause 8.3, so the shop operates as a build-to-print manufacturer.
How is process capability proven?
In short, With SPC control charts on key characteristics. On a representative length characteristic of 76.1–76.5 mm, the chart showed Cpk = 1.851 (one characteristic on one part, not a blanket capability claim) across 25 subgroups, against a target of Ppk ≥ 1.67 initial for key characteristics and ≥ 1.33 for general ones — a stable process, not a passing sample.
How do you prevent mixed-lot material scrap?
In short, Every incoming lot is XRF-checked against its mill certificate before it reaches a machine, so a wrong alloy is caught at the door rather than after machining. That single step removes a whole class of scrap that a buyer would otherwise pay for in rejects.
Can parts be traced back to the raw material?
In short, Yes. The MES/ERP system records material source, process parameters, machine data, batch, operator, and inspection results for every lot.
What quality documents ship with the parts?
In short, A first-article inspection report, a CMM dimensional report, SPC control charts, and the material certificate can ship with the parts. The documents move your incoming inspection from re-measuring everything to confirming the record — a direct saving in the supplier-management bucket.
What does Cpk tell a buyer about quality?
In short, Cpk measures how far the process mean sits from the nearest tolerance limit, in standard deviations. A Cpk of 1.33 is the common minimum for stable production, 1.67 is the key-characteristic bar, and 2.0 means rejects are effectively designed out.
How does a buyer verify material without visiting the floor?
In short, Ask for the XRF read against the mill certificate for the lot, plus the traceability record. A wrong alloy looks identical to a right one until it fails, so the XRF check at incoming — and the record of it — is the verification that closes the loop between the certificate and what is actually on the machine.
Metal Parts China Quality — Related Pages
Continue reading: Metal Parts China Factory · Metal Parts China Services · Resources for sourcing Metal Parts China
Standards referenced on this page
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- ISO 14001 — Environmental management systems — Requirements with guidance for use
- IATF 16949:2016 — Automotive quality management system standard